What needed solving
A line handling multiple bottle-label variants needed consistent checks for missing, reversed or wrong labels and absent rear batch codes.
The front presentation label and rear label/code area needed separate camera views as each bottle passed the labeler.
How Qualitas solved it
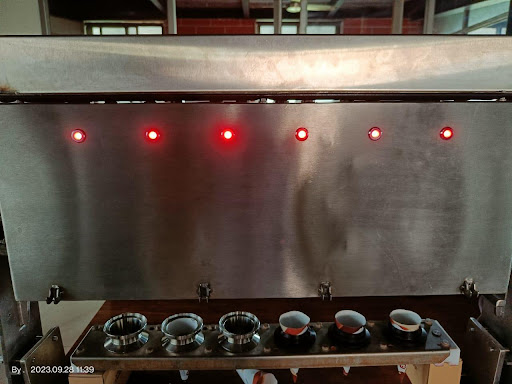
A bottle sensor triggers two area-scan cameras, each with a fixed-focus lens and dedicated bar light. Vision software checks the active variant, records the image and result, and sends separate pass/fail signals to the line controls.
Front label and rear code area, checked together
A wrong, reversed or absent label can move beyond the labeler before an operator can consistently check it. This station gives the brewery a fixed inspection point: the front label and rear label/batch-code area are checked before a pass or fail signal returns to the line.
The front camera checks whether the body label is present, correctly oriented and appropriate for the selected product. The rear camera checks the rear label and the presence of the batch code. These are checks of the bottle’s labels and code area; they do not inspect the beer inside the bottle.
| Check | Purpose |
|---|---|
| Label presence | Confirm that a label is present in the expected region. |
| Label orientation | Flag a reversed or wrongly oriented label. |
| Selected variant | Check the label against the active bottle-label combination. |
| Rear batch-code presence | Confirm that the batch code is present on the rear face. |
Two camera views, triggered by the bottle
The bottle crossing a sensor starts the inspection. Each camera captures its respective face under a dedicated bar light. The software checks the image against the inspection regions for the selected variant and produces separate pass and fail outputs for the line controls.
Qualitas supplied the imaging and inspection system: two area-scan cameras, fixed-focus lenses, bar lighting, an industrial computer, vision software, operator application and controls interface. Camera and light mounts hold the views in a repeatable position around the bottle path.
Separate 24 V DC pass/fail signals provide the interface for the downstream line response.
A recipe for each bottle-label combination
The project covered 14 bottle-label variants. An authorised operator selects the active variant before inspection, pairing the correct regions and label expectations with the product on the line. The application provides start and bypass controls, displays the inspected image and highlights failed components.
A record behind each decision
The operator sees the pass/fail result and count. Pass and fail images are retained on the computer, while the inspection record includes date, time, variant and result. These records give production and quality teams a practical way to review a decision after the bottle has moved on.
Label presence, orientation, variant matching and rear batch-code presence become one repeatable workflow: select the product, inspect both faces, review the result and retain a record.
Share your bottle and label variants, line speed, labeler layout, available sensor/PLC signals and examples of the label errors you need to stop. We can assess camera positions, lighting and the decision interface around your line constraints.
Request project details