Micron-level accuracy
Non-contact optical measurement holds tolerances that replace calipers, CMMs, and profilometers on the line.
Calipers, profilometers, and CMMs only sample a fraction of production. Vision-based gauging measures dimension, thickness, height, area, and volume on every part, inline, at full line speed — with a logged reading you can trend.
A profilometer or CMM check every few minutes catches a problem only if it happens to land on a sampled part. Thickness, bore diameter, gap, and fill level can drift for hundreds of parts before the next sample flags it.
Qualitas EagleEye® measures every part inline — 2D dimensional checks or full 3D height/area/volume where geometry demands it — logging a per-part reading so drift is caught the moment it starts, not after a batch has already gone out.
Non-contact optical measurement holds tolerances that replace calipers, CMMs, and profilometers on the line.
Every part is measured at production speed — not a 5% CMM sample with drift undetected in between.
Every measurement is logged, giving you real Cpk/Ppk from 100% of parts instead of batch-level pass/fail.
 ENGINEERING TOOLSCASE STUDY
 AUTOMOTIVE INDUSTRIESCASE STUDY
 ENGINEERING TOOLSCASE STUDY
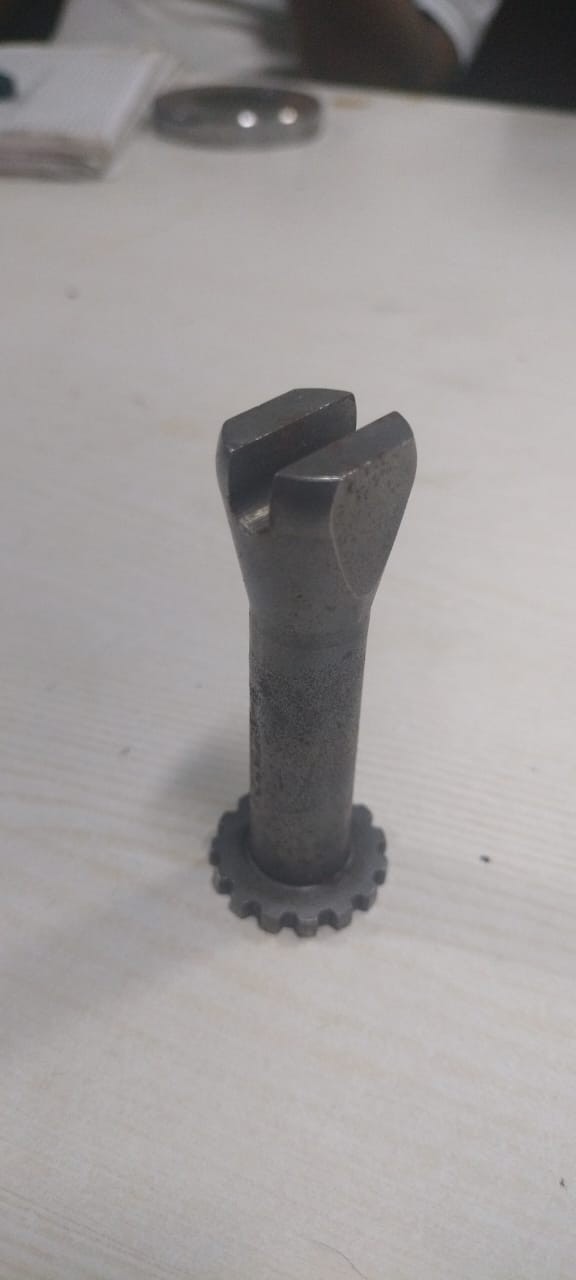 AUTOMOTIVE INDUSTRIESCASE STUDY
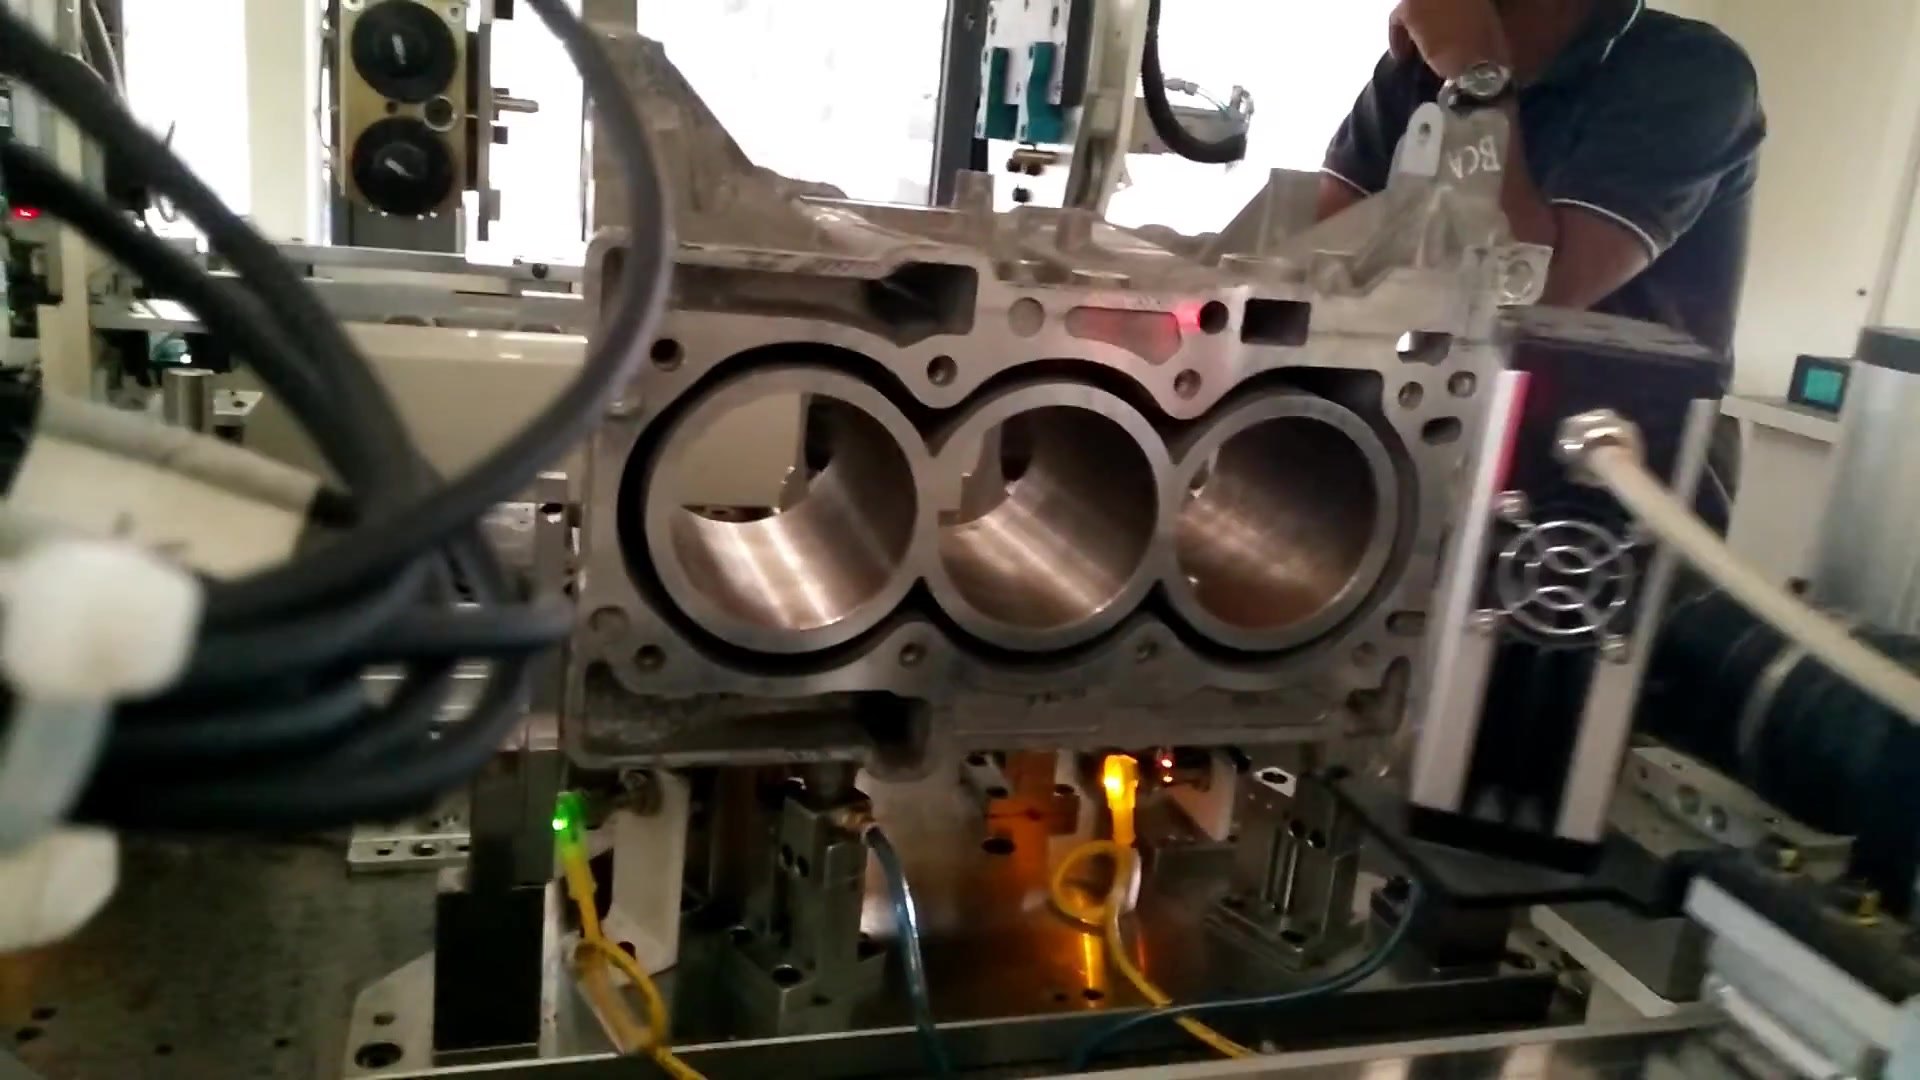 AUTOMOTIVE INDUSTRIESCASE STUDY
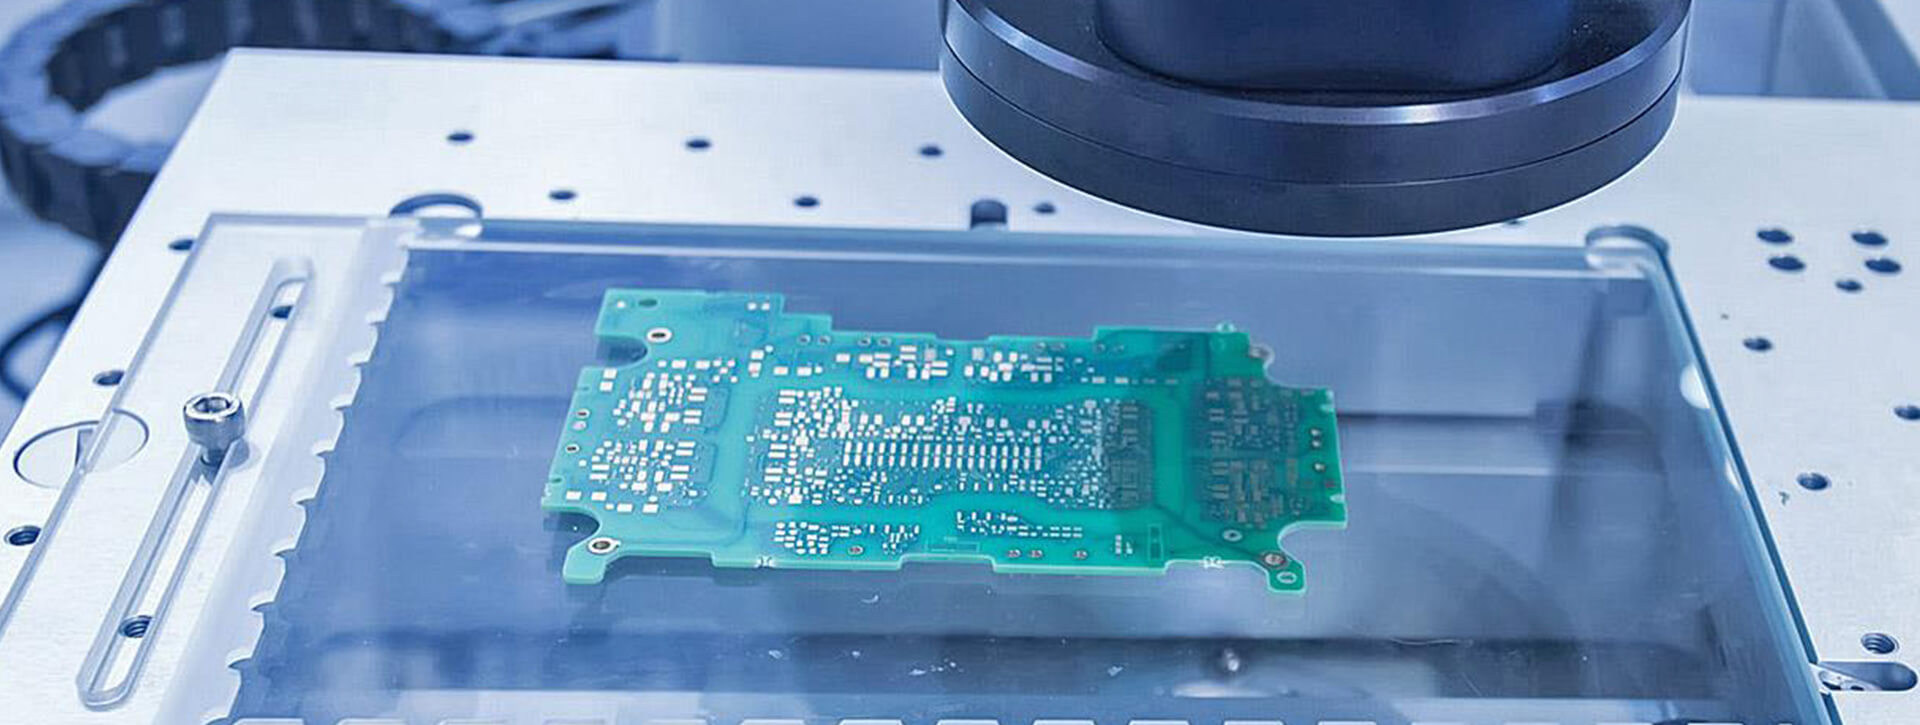 CONSUMER ELECTRONICSAPP NOTE
Small edge changes and inconsistent presentation can affect measurements of ferrite core dimensions.
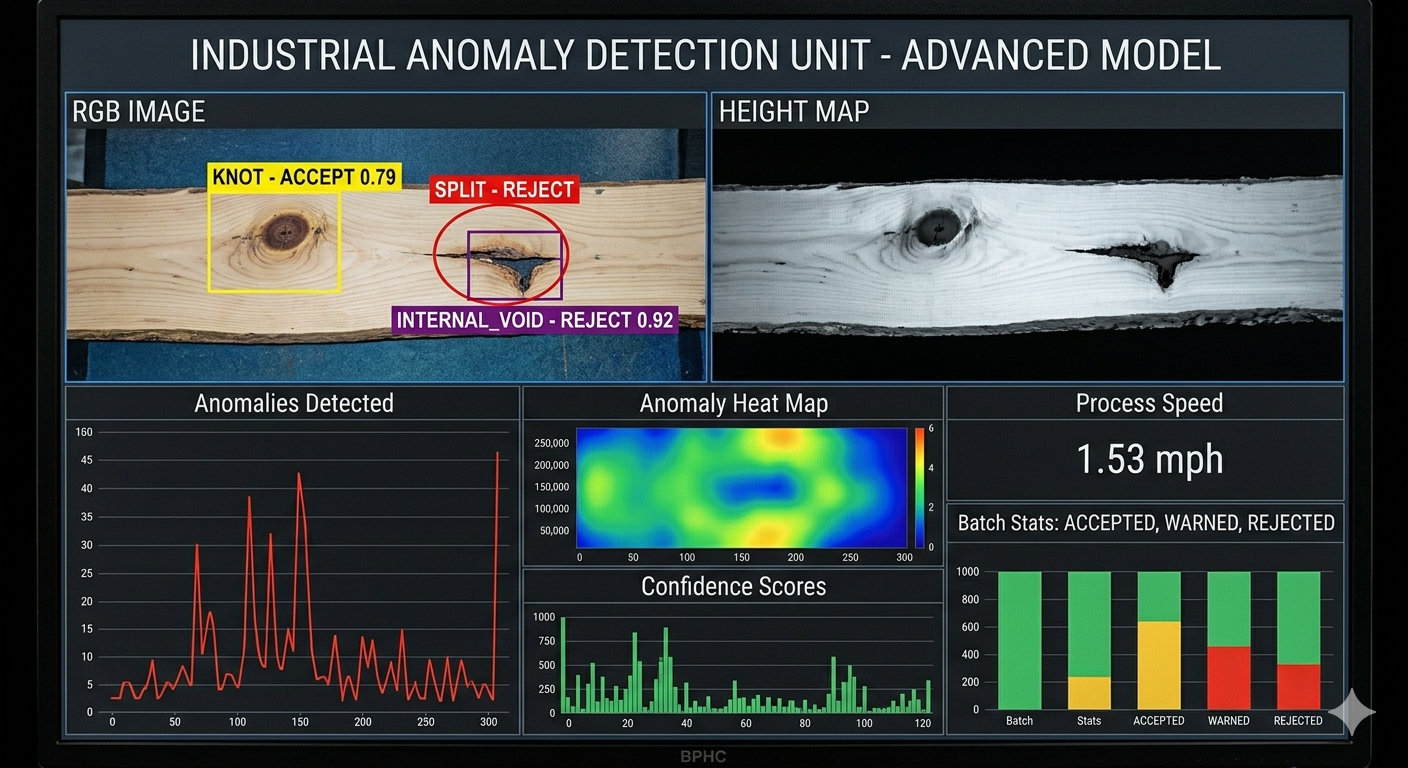 INDUSTRYAPP NOTE
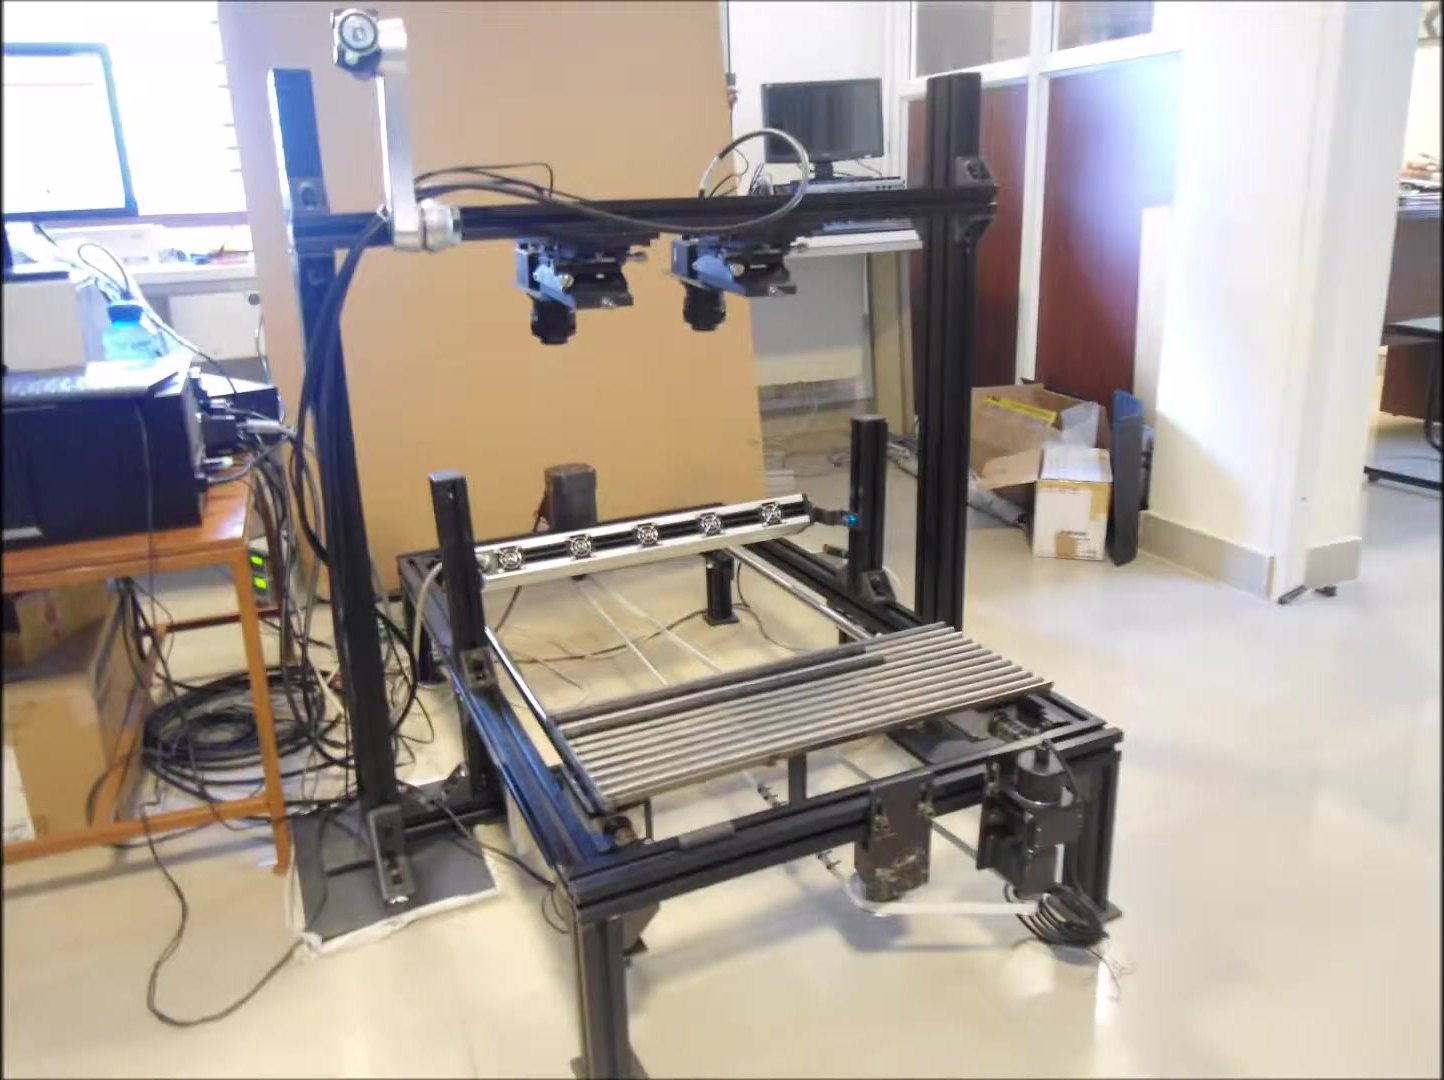
Laser triangulation profilometry combined with a multi-camera array and deep-learning defect classification for inline dimensional measurement and knot, crack, hole, and edge-damage detection on wood planks at conveyor speed — with defect-zone marking to support cut optimisation.
Tell us your tolerance and part — we'll share a feasibility view and the accuracy you can expect.